 Post by
The majority of waste losses in tempering plants are due to a single cause: The edge of the glass entering the furnace is unfinished. This article explains why this happens and how the break-in period prevents it.
What happens to the glass during tempering?
In the tempering process, the glass is heated to approximately 620–650 °C, then cooling air is rapidly blown onto its surface. The surface cools and contracts faster than the inside; the interior remains hot and expanded.
Ultimately, glass pressure on the surface, tensile stress on the inside This is precisely what makes the glass 4–5 times stronger than normal glass: the pressure on the surface makes it difficult for external impacts to initiate cracks.
So why does it explode?
A cut edge of glass appears smooth to the naked eye. However, at the microscopic level, the situation is different: the cutting process runs along the edge. micro-notch and cracks They leave it. These don't normally cause problems.
In tempering, the stress introduced becomes a force that enlarges this micro-crack. When the crack reaches a critical size, the glass releases itself — and when tempered glass breaks, it shatters into thousands of tiny pieces.
The insidious part is this: glass doesn't always shatter in the furnace. Sometimes it comes out intact, is packaged, shipped, and then spontaneously breaks in the field—even weeks after assembly. These delayed breakages are both costly and damaging to reputation.
How does the break-in period solve this problem?
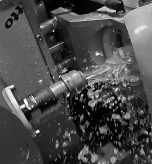
Edge processing physically removes the layer of material containing microcracks. Once the edge is smooth, there is no longer a starting point for thermal stress to amplify.
There is an important distinction here: Bright blasting is not required for tempering. In double-glazed units where the edge will not be visible, seaming is often sufficient. The aim is not aesthetics, but to prevent the onset of cracks.
The difference between different types of break-in processes
- Deburring (seaming/arrissing): It removes the sharpness from the edge. Minimum requirement in tempering and insulating glass lines.
- Straight break-in period: It brings the edge to a smooth surface, leaving the edge matte.
- High-gloss polishing: It polishes the edges. It is used on products where the edges are visible, such as shower enclosures and table glass.
- Corner and radius: It breaks or rounds sharp edges, reducing the risk of injury during handling.
A common production planning mistake.
The most costly mistake is setting up the order of operations incorrectly. No further processing can be done to the glass after tempering. — Drilling, cutting, edge finishing, none of that. Touching tempered glass with a drill will shatter it.
The correct order is:
- Cut
- Edge finishing (grinding/polishing)
- Drilling, countersinking, shaped cutting.
- Washing
- Tempering
The glass, having entered the furnace, is now in its final form.
What else is changing in insulating glass production?
In insulating glass units, the effect of an unprocessed edge manifests itself in a different way: the spacer and sealant cannot make full contact with the glass. The result is that, over the years, the unit absorbs moisture and condensation develops from the inside. This means a replacement under warranty.
Summary
Every piece of glass entering the tempering furnace must have its edges finished. This isn't a quality preference, but a physical requirement of the process. If you have an unexplained high waste rate, the first place to look is edge preparation.
Glass grinding and polishing machines You can get detailed information about it or DKDT series You can check it out.